Skip to content
ABOUT ECENTIC LIFESCIENCE

Advancing health through science, quality & precision.

ECENTIC LIFESCIENCE is a global, multi-division life sciences company headquartered in India, delivering pharmaceutical, nutritional and biosecurity solutions across international markets.

WHY CHOOSE ECENTIC LIFESCIENCE
MANUFACTURING & QUALITY

Excellence

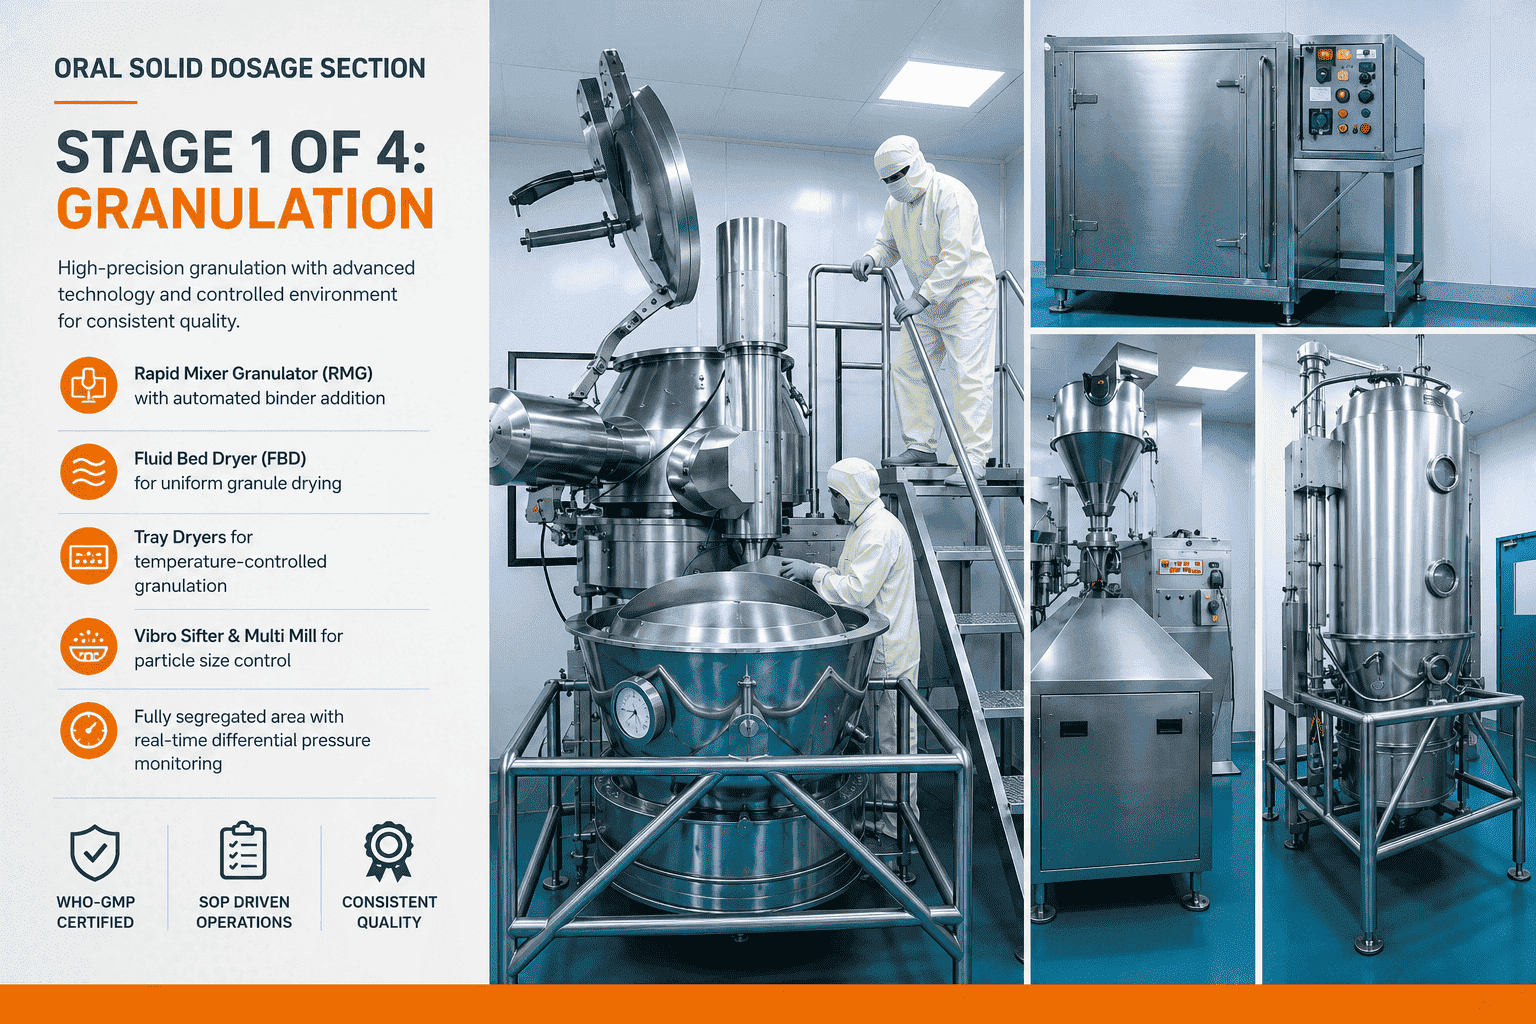
Oral solid dosage granulation and pharmaceutical manufacturing

Our products are manufactured at advanced pharmaceutical manufacturing facilities equipped with WHO-GMP-certified and cGMP-compliant facilities, specialized manufacturing capabilities and robust quality systems to support consistent product quality, process control and reliable supply.
CONTROLLED & VALIDATED

Manufacturing

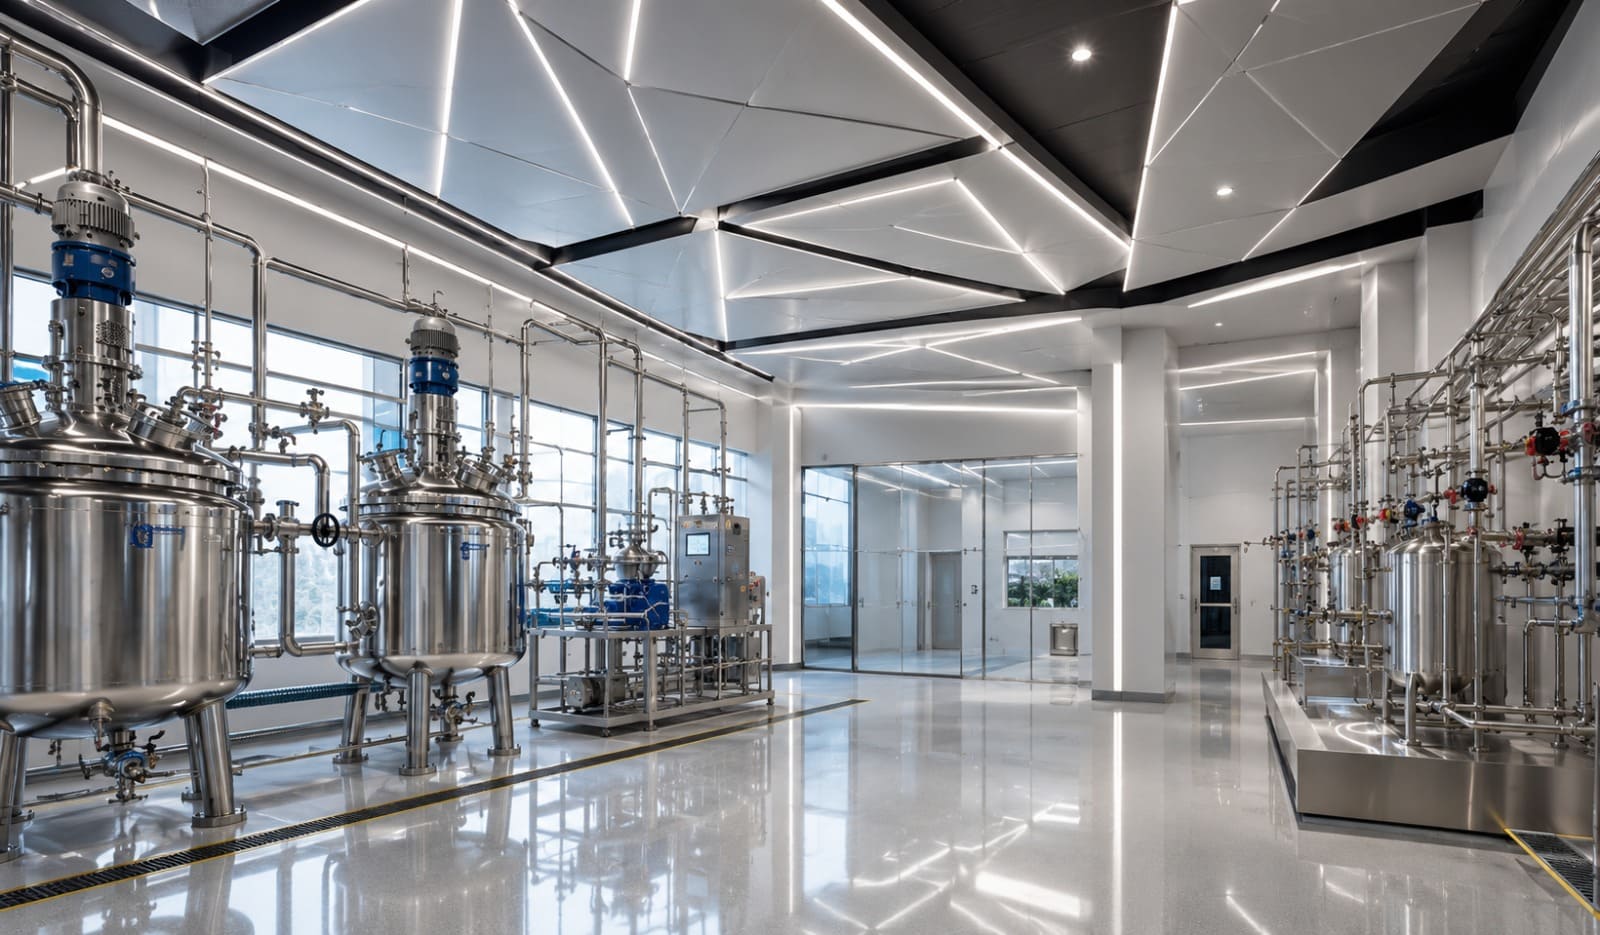
Pharmaceutical manufacturing facility

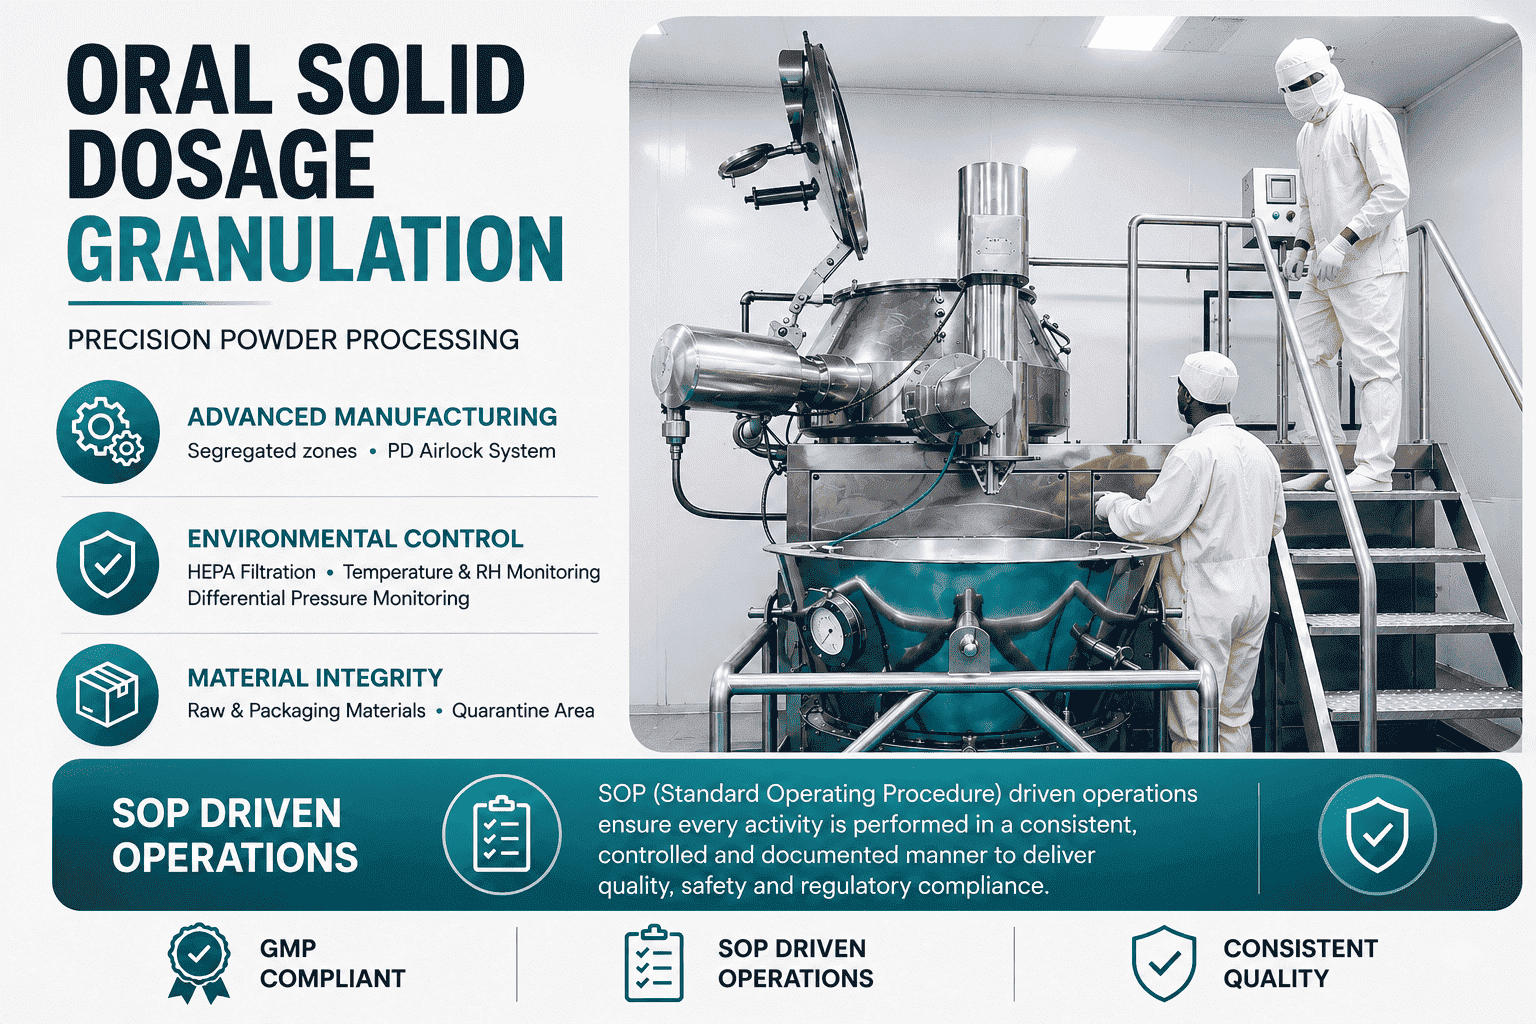
Our products are manufactured under controlled production environments equipped with fresh-air systems, terminal HEPA filtration and continuous monitoring of temperature, relative humidity and differential pressure, where applicable.

Process validation, cleaning validation and hold-time studies support controlled, consistent and reproducible manufacturing processes.

TRACEABLE & SECURE

Processes

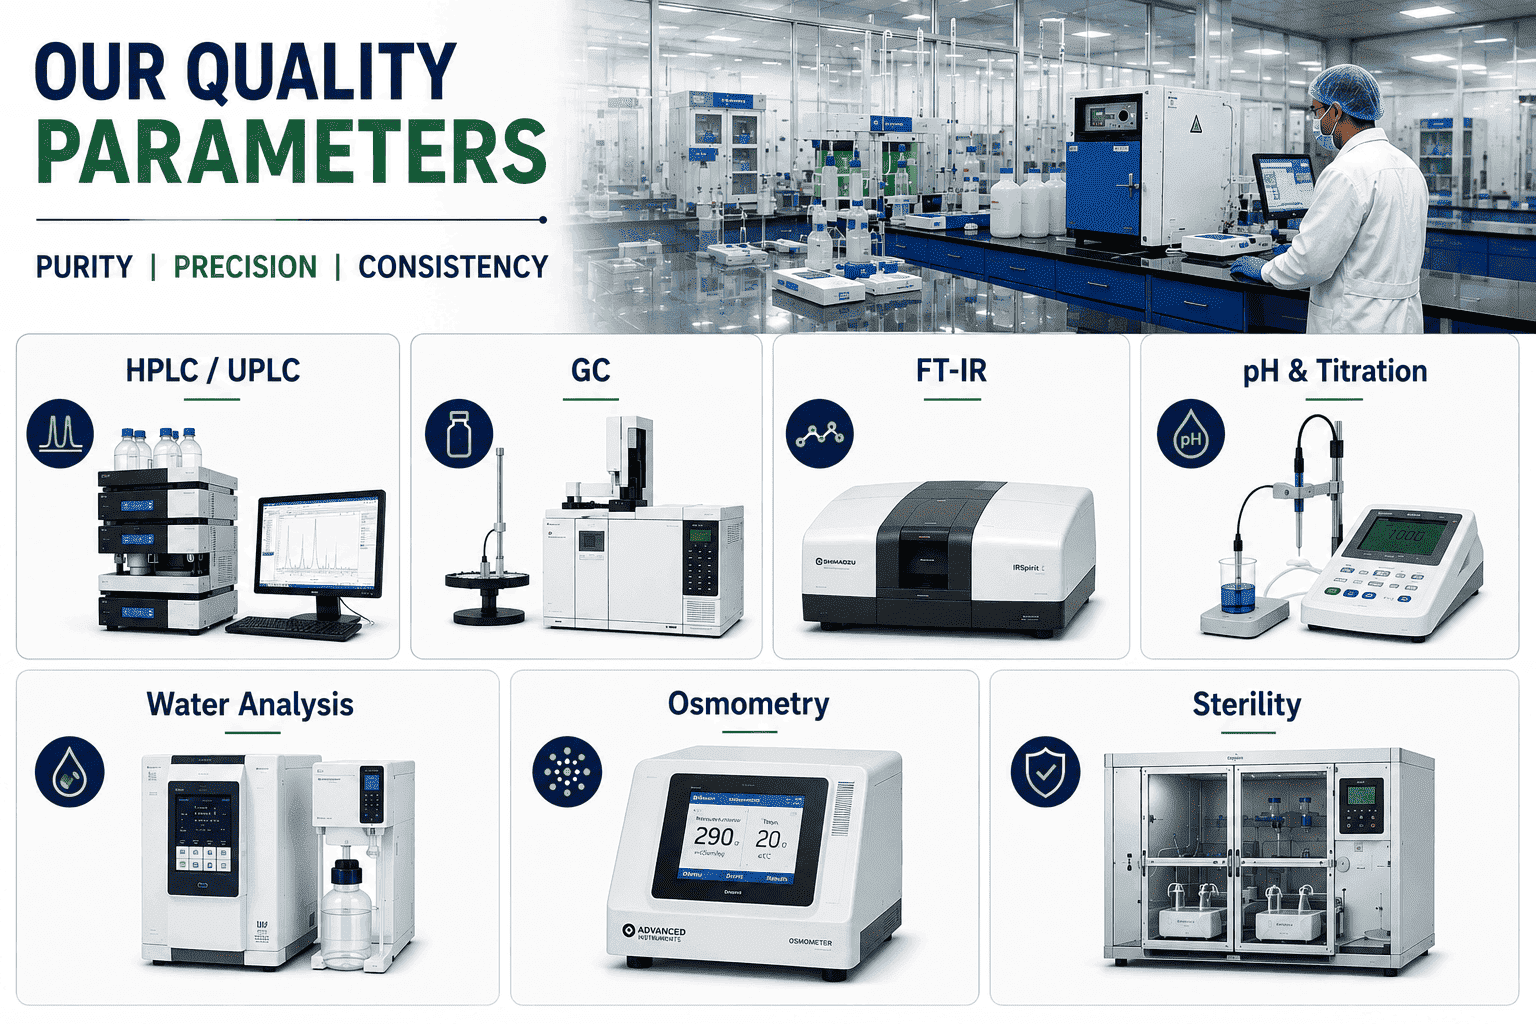
Pharmaceutical analytical quality testing

Electronic Batch Manufacturing Records (BMRs) support structured documentation, process control and end-to-end batch traceability across manufacturing operations.

ANALYTICAL QUALITY

Assurance

Pharmaceutical analytical quality testing

Our analytical quality systems support comprehensive evaluation of raw materials, in-process materials and finished products through established analytical techniques and quality-control procedures.

Analytical Quality Assurance

ANALYTICAL TECHNIQUES CORE QUALITY TESTING
Analytical Technique
Key Parameters
Quality Purpose
HPLC / UPLC
Assay, impurities & related substances
Quantitative determination of active ingredients and assessment of related substances and impurities.
GC
Residual solvents
Determination of residual solvents against specified limits.
FT-IR
Material identification
Identification of raw materials and active pharmaceutical ingredients through characteristic infrared spectra.
pH & Titration
pH and chemical characteristics
Evaluation of specified chemical characteristics and, where applicable, concentration-related parameters.
Water Analysis
Conductivity, TOC & microbial quality
Assessment of purified water/WFI quality against specified chemical and microbiological requirements.

Injectable-Specific Quality Testing

ANALYTICAL TESTING INJECTABLE QUALITY
Analytical Test
Key Parameters
Quality Purpose
Osmometry
Osmolality
Determination of osmolality to support compliance with applicable product specifications.
Sterility Testing
Viable microorganisms
Evaluation of finished injectable products for compliance with applicable sterility requirements.
Bacterial Endotoxin Testing
Endotoxins
Determination of bacterial endotoxin levels against applicable specification limits.
Particulate Matter
Visible & subvisible particles
Assessment of particulate matter in injectable products against applicable pharmacopeial requirements.

Where required, selected products may undergo independent third-party analytical testing at qualified external laboratories, providing an additional level of analytical verification, quality assurance and confidence in product quality.

SPECIALIZED MANUFACTURING CAPABILITIES

Pharmaceutical Injectable Solutions.

Our human pharmaceutical injectable solutions are manufactured at specialized pharmaceutical facilities using IP-compliant ingredients, where supported by applicable specifications and documentation, along with stringent quality-control systems and controlled manufacturing processes.

Purity | Precision | Consistency
25+
EXPORT MARKETS

Serving pharmaceutical markets across Asia, Africa, CIS and Latin America.